Rice Color Sorting vs. Rice Grading is an important comparison for rice mill operators who want to improve product quality, reduce processing losses, and select suitable equipment. Although both processes help produce more consistent rice, they serve different purposes and rely on different technologies.
Rice color sorting removes visually defective grains using optical detection, while mechanical rice grading separates kernels according to physical dimensions, such as length and thickness. One focuses on appearance, while the other controls grain-size distribution.
For rice processors, this distinction directly affects equipment selection. A mechanical grader can separate broken kernels from whole rice, but it cannot reliably identify yellow grains with normal dimensions. Likewise, an optical sorter can remove discolored kernels but may not replace a dedicated length grader.
It is also important to distinguish mechanical grading from commercial rice quality grading, which can include several criteria beyond kernel size.
Understanding how these technologies differ helps processors avoid unnecessary investments and design more effective production lines.
Understanding Rice Color Sorting and Rice Grading
Before comparing equipment, it is useful to understand how each process works and what it can realistically achieve.
How Does Rice Color Sorting Work?
Rice color sorting is an automated optical inspection process that identifies unwanted kernels based on detectable differences in appearance.
A typical rice color sorter uses controlled lighting, cameras, image-processing software, and pneumatic ejectors.
As rice passes through the inspection area, cameras capture images of individual kernels. The system analyzes their visible characteristics and determines whether they meet the configured acceptance criteria.
When a defective kernel is detected, a precisely timed air jet redirects it into a separate reject stream.
Depending on the optical system and sorting settings, detectable defects may include:
- Yellow or darkened kernels
- Black or spotted grains
- Red or differently colored rice
- Visibly chalky kernels
- Certain damaged or discolored grains
- Visually distinguishable foreign materials
Advanced optical sorters may also analyze grain shape, allowing them to identify selected broken or irregular kernels.
However, shape recognition does not automatically make an optical sorter equivalent to a mechanical length grader. Actual separation performance depends on equipment capabilities and material characteristics.
Similarly, chalky rice detection depends on the degree of chalkiness, optical contrast, and inspection conditions.
The primary objective is to improve visual quality while minimizing the rejection of acceptable rice.
How Does Mechanical Rice Grading Work?
Mechanical rice grading separates kernels according to physical dimensions.
Two common grading methods are length grading and thickness grading.
Length grading commonly uses indented cylinders to separate shorter kernels from longer ones. It is especially useful for dividing rice into whole-grain and broken-grain fractions.
Thickness grading uses screens or appropriately sized openings to separate grains according to their thickness.
These processes help rice mills produce more uniform size fractions and manage broken-rice content.
Unlike optical inspection, conventional mechanical graders do not primarily evaluate grain color or surface discoloration.
Consequently, yellow rice and acceptable white rice of similar dimensions may remain in the same fraction.
This is why the two technologies often perform complementary roles in commercial rice processing.

Rice Color Sorting vs. Rice Grading: Key Differences
The main differences involve separation criteria, equipment operation, and their influence on finished-rice quality.
Comparison of Rice Sorting and Grading Equipment
| Comparison Factor | Rice Color Sorting | Mechanical Rice Grading |
| Primary purpose | Remove visually unwanted kernels | Separate rice by physical dimensions |
| Separation criteria | Color, brightness, detectable surface features and shape | Length or thickness |
| Main technology | Cameras, lighting, image processing and air ejectors | Indented cylinders or mechanical screens |
| Yellow rice removal | Suitable when discoloration is detectable | Not specifically designed for this task |
| Broken rice separation | Possible with suitable shape recognition | Main application of length grading |
| Chalky rice separation | Possible under suitable optical conditions | May separate some thin or immature kernels |
| Typical output | Visually improved accepted rice | Different grain-size fractions |
| Main performance concern | Defect removal and good-rice carryover | Size separation efficiency |
| Typical application | Optical quality control | Broken-rice and size classification |
Different Separation Principles
Consider a rice batch containing whole white kernels, whole yellow kernels, and broken white kernels.
A length grader separates grains according to length. Therefore, it can remove much of the broken rice, but yellow whole kernels may remain in the accepted fraction.
An optical sorter can subsequently identify yellow kernels through their visible characteristics.
This example demonstrates why equipment should be selected according to the actual defect being targeted.
Different Operating Requirements
Mechanical graders rely on physical separation surfaces. Their operation requires attention to screen condition, cylinder configuration, wear, and material distribution.
Optical sorters depend on stable feeding, clean cameras, controlled lighting, compressed air, and correctly configured sorting parameters.
Both require maintenance, but their operating priorities differ.
For buyers, the most important consideration is whether the equipment can consistently meet the required quality specification under realistic production conditions.
How Rice Color Sorting and Grading Work Together in Rice Milling
Rice grading and optical sorting are frequently integrated into commercial milling lines.
Instead of competing with one another, they address different quality requirements at different processing stages.
Typical Rice Milling Process
A simplified production sequence may include:
- Pre-cleaning: Removes larger impurities and foreign materials.
- Dehusking: Removes the outer husk from paddy rice.
- Paddy separation: Separates unhusked grains from brown rice.
- Whitening and polishing: Removes bran layers and improves surface appearance.
- Mechanical grading: Separates whole rice from broken or differently sized fractions.
- Optical sorting: Removes selected discolored or visually defective kernels.
- Final inspection and packaging: Verifies product quality before distribution.
This sequence is illustrative. Actual equipment arrangements vary according to rice variety, plant design, processing capacity, and finished-product requirements.
Why Grading Often Comes Before Optical Sorting
Mechanical grading can create more uniform material streams before optical inspection.
For example, a rice mill may separate whole rice from broken rice and process each fraction using different optical sorting settings.
This allows operators to apply quality requirements suited to each product category.
Premium whole rice may require stricter visual consistency, while broken rice sold for other applications may have different acceptance criteria.
More uniform feeding can also simplify downstream sorting adjustments, although the actual benefits depend on equipment design.
Can Optical Sorting Replace Mechanical Grading?
In some applications, optical sorting can assist with broken-rice separation.
Modern image-processing systems may recognize differences in kernel shape and length. However, this capability depends on the machine’s installed inspection technology.
Mechanical length graders remain valuable when processors require consistent separation of multiple broken-rice fractions.
Therefore, buyers should not assume that every optical sorter can replace mechanical grading equipment.
The appropriate decision depends on the required separation accuracy, rice characteristics, and results from representative sample testing.
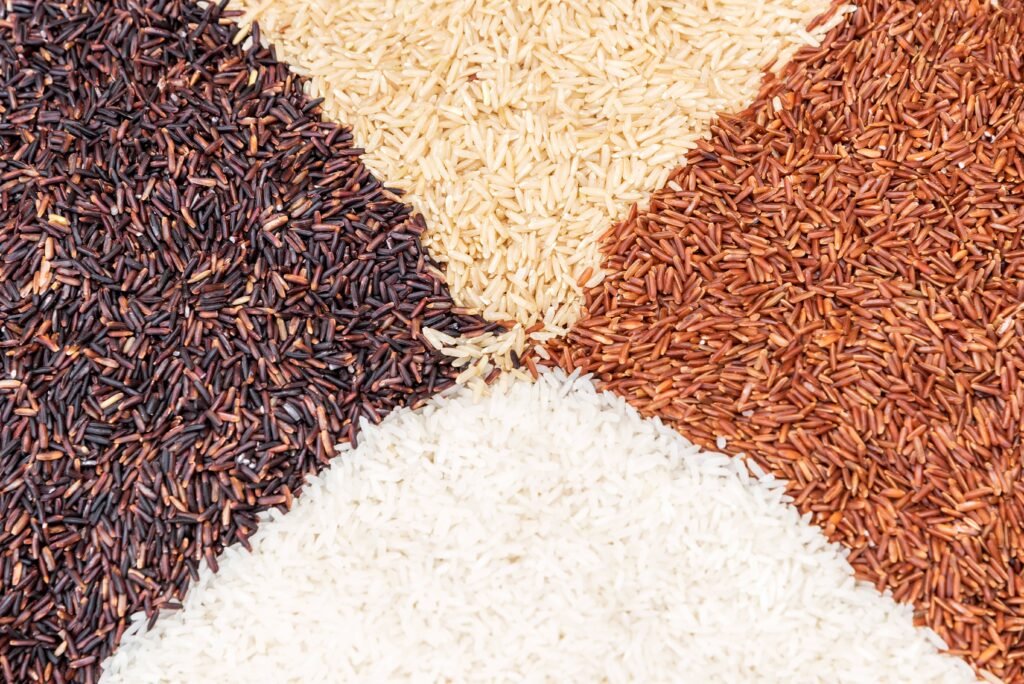
How to Choose the Right Rice Sorting or Grading Equipment
Choosing between optical sorting and mechanical grading starts with identifying the main quality problem.
A machine with more advanced technology is not necessarily the best solution if it addresses the wrong separation requirement.
Equipment Selection Based on Processing Problems
| Processing Problem | Recommended Equipment or Approach |
| Excessive broken rice | Rice length grader |
| Yellow or dark kernels | Rice color sorter |
| Inconsistent grain thickness | Rice thickness grader |
| Visually inconsistent finished rice | Rice color sorter |
| Broken rice and discoloration together | Combined grading and optical sorting |
| Excessive good rice in optical rejects | Sorting optimization or reject recovery |
| Multiple commercial size fractions | Suitable mechanical grading equipment |
This comparison provides a starting point. Final selection should consider the buyer’s actual rice samples and quality targets.
Important Performance Indicators for Buyers
Before purchasing a rice color sorter, processors should evaluate three key indicators.
1. Defect Removal Rate
This measures the proportion of targeted defective kernels successfully removed from the incoming material.
A higher removal rate can improve finished-product appearance. However, results depend on the types and visibility of defects.
2. Good-Rice Carryover
Good-rice carryover refers to acceptable kernels that enter the rejected stream.
Excessive carryover reduces usable product recovery and may increase operating costs.
Therefore, buyers should evaluate defect removal and acceptable-rice loss together rather than focusing on rejection performance alone.
3. Actual Processing Throughput
Throughput represents the quantity of rice processed over a given period, commonly expressed in tons per hour.
However, practical capacity depends on rice variety, incoming defect concentration, feeding conditions, and required output quality.
A machine’s advertised capacity should not be treated as guaranteed performance for every application.
Why Sample Testing Matters
Representative sample testing is one of the most useful steps before equipment selection.
Buyers should provide rice that reflects normal production conditions, including typical discoloration, broken kernels, and impurities.
A meaningful sorting trial should record:
- Incoming material quality
- Processing throughput
- Defect concentration in the accepted product
- Remaining acceptable rice in the reject stream
- Sorting stability during continuous operation
Whenever possible, these measurements should be compared against clearly defined acceptance criteria.
This approach helps buyers assess equipment suitability using measurable results rather than specifications alone.
Improving Rice Quality, Recovery, and Processing Value
The commercial value of rice sorting equipment extends beyond its initial purchase price.
Processors should evaluate how different technologies affect product consistency, usable yield, operating expenses, and market requirements.
Improving Finished-Rice Consistency
Mechanical grading helps maintain consistent grain-size fractions, while optical sorting improves visual uniformity.
Combining these processes can help facilities meet customer specifications covering both broken-rice content and visible defects.
However, optical sorting cannot guarantee complete removal of food safety hazards or contaminants that lack detectable optical characteristics. Appropriate testing and quality-control procedures remain essential.
Reducing Product Loss
Efficient rice processing requires protecting acceptable kernels while removing unwanted material.
Mechanical grading allows broken rice to be collected as a separate commercial fraction.
Optical sorting can reduce selected visual defects, but incorrect settings may increase good-rice carryover.
Where justified, secondary reject sorting can help recover acceptable grains from the rejected stream.
The financial benefit depends on recovered product value, operating costs, and the additional equipment required.
Evaluating Long-Term Equipment Value
When calculating investment value, rice processors should consider more than machine capacity.
Important factors include product recovery, stable output quality, maintenance requirements, compressed-air consumption, and compatibility with existing machinery.
For facilities already achieving acceptable broken-rice percentages but struggling with discoloration, optical sorting may offer a more targeted improvement.
For mills primarily experiencing inconsistent grain-size fractions, upgrading mechanical grading may be the more appropriate investment.
Ultimately, the best equipment configuration is the one that meets measurable product requirements with acceptable operating costs and material losses.
Frequently Asked Questions About Rice Color Sorting and Rice Grading
1. What is the main difference between rice color sorting and rice grading?
Rice color sorting uses optical inspection to remove visually unwanted kernels. Mechanical rice grading separates grains according to dimensions such as length or thickness. Both improve product consistency, but they address different quality characteristics.
2. Can a rice color sorter remove broken rice?
Some optical sorters can identify broken kernels using shape-recognition technology. However, performance depends on the machine configuration and rice characteristics. Dedicated length graders remain useful for separating multiple broken-rice fractions.
3. Is mechanical grading necessary before rice color sorting?
Not always. Mechanical grading commonly precedes optical sorting, but the optimal processing sequence depends on plant layout, raw material characteristics, and finished-product specifications.
4. Which equipment is better for removing yellow rice?
An optical rice color sorter is generally more suitable because yellow kernels can be identified through visible color differences. Conventional mechanical grading does not specifically target discoloration.
5. Can optical sorting improve rice quality?
Yes. Optical sorting can remove selected visually defective kernels and improve appearance consistency. However, performance depends on detection capabilities, material condition, and sorting settings.
6. Can rice grading and color sorting operate in the same production line?
Yes. Many commercial rice mills use both technologies. Mechanical grading separates size fractions, while optical sorting removes selected visual defects, providing complementary quality-control functions.
7. What should buyers check before purchasing a rice color sorter?
Buyers should evaluate representative sorting samples, actual throughput, defect removal, good-rice carryover, operating requirements, and compatibility with existing equipment. Testing against defined product specifications provides the most useful basis for selection.
Conclusion: Choosing the Right Rice Processing Solution
The comparison of Rice Color Sorting vs. Rice Grading shows that these technologies perform different but complementary functions.
Mechanical grading controls grain-size distribution and broken-rice fractions. Optical sorting improves visual consistency by identifying and rejecting selected unwanted kernels.
For commercial rice mills, combining both technologies may provide more comprehensive quality control. However, the most suitable configuration depends on incoming rice characteristics, production capacity, and finished-product requirements.
At PolySorter, we provide rice color sorting solutions for commercial rice processing applications. Explore our rice sorting equipment or contact our team to discuss your raw materials, quality targets, and production requirements.